Why It Matters
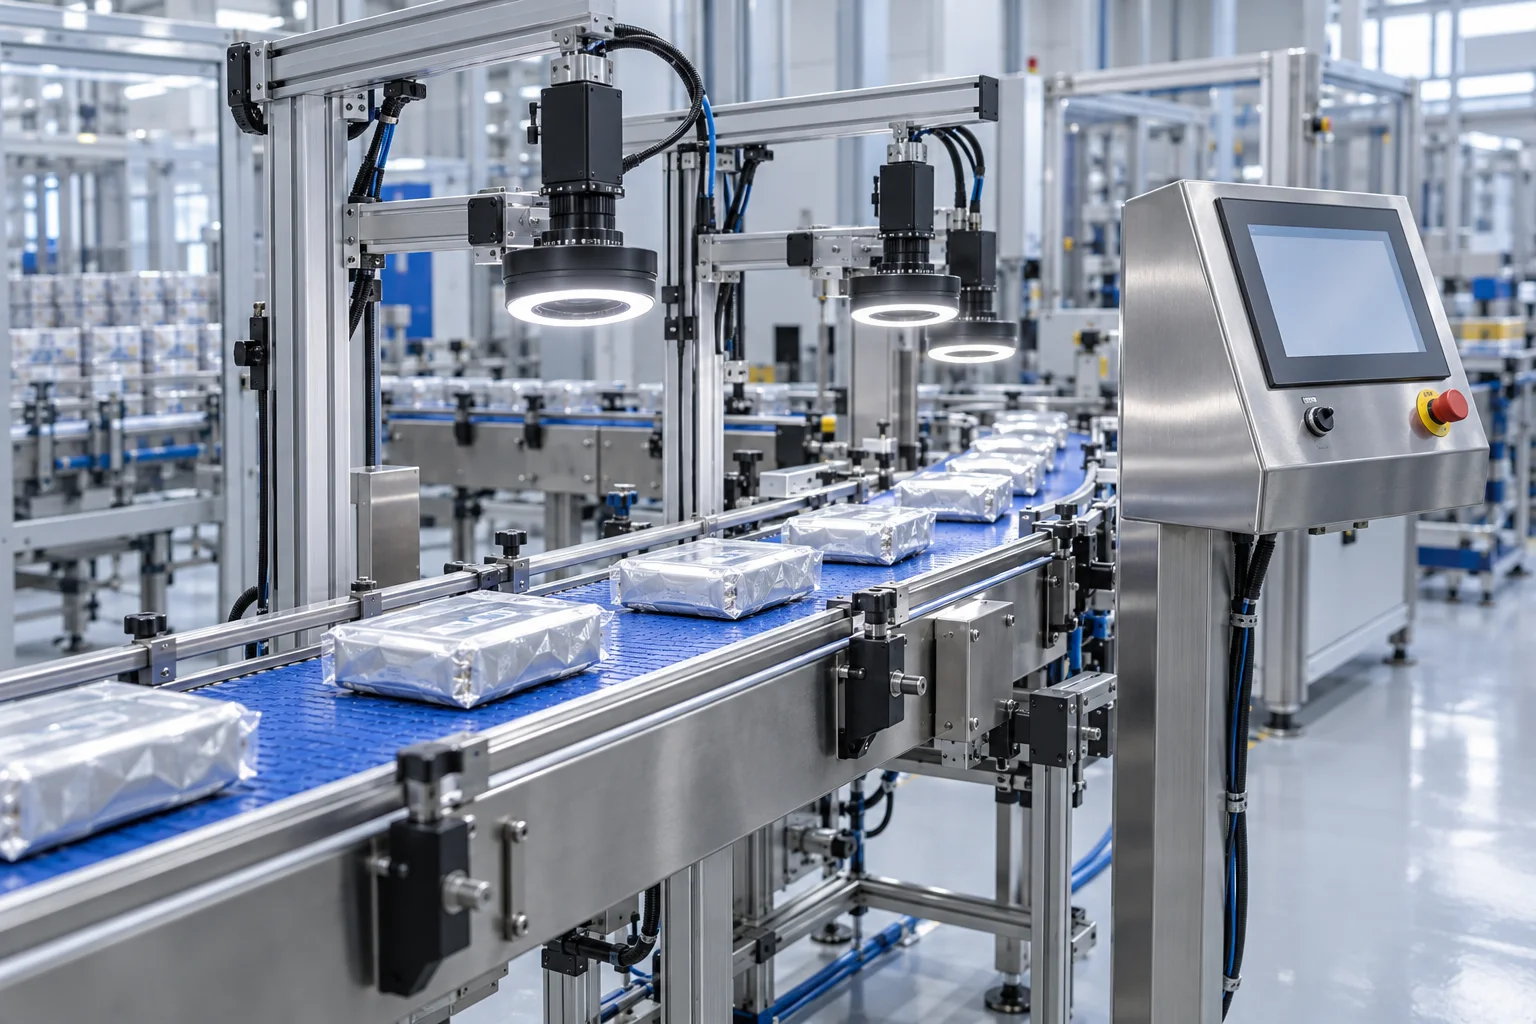
Vision systems are becoming part of the process conversation. They can reveal drift earlier, verify changes and give operators a clearer reason for each reject.
Key Data Points
| Topic | Planning Note |
|---|---|
| Inspection examples | Seal, label, fill level, code and appearance |
| Useful result | Earlier detection of process drift |
| Integration point | PLC, HMI, reject confirmation and production data |
Start with a defect definition
A camera cannot improve a process until the team agrees what a defect looks like and what variation is acceptable.
Control light before adding complexity
Stable lighting, part presentation and trigger timing often matter more than adding another algorithm.
Turn rejects into information
Reject images and reason codes help production teams separate material variation, setup error and machine drift.
Protect line speed
Inspection should be tested with real product, real speed and realistic variation so false rejects do not become the new bottleneck.
Plan the recipe lifecycle
Every new SKU needs a controlled recipe, acceptance samples and an owner for future updates.