Why It Matters
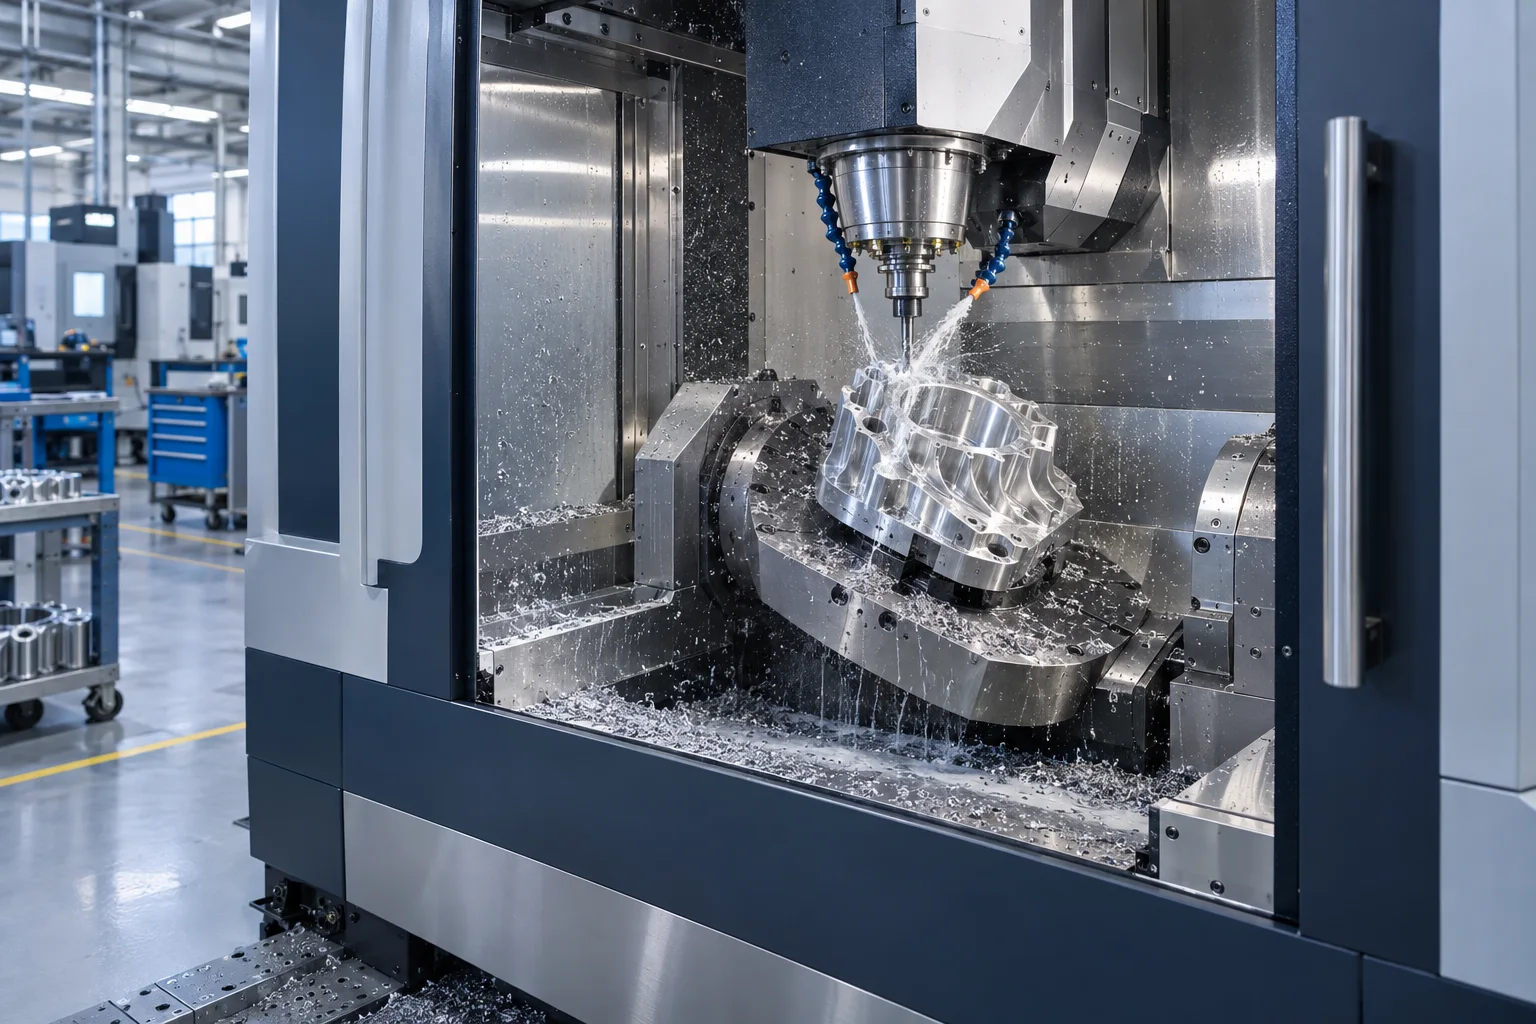
The most capable machining center still loses value when setup, chip removal or tool access slows the operator. Uptime begins with practical access around the machine.
Key Data Points
| Topic | Planning Note |
|---|---|
| Uptime lever | Setup reduction and reliable chip control |
| Design input | Part family, tool strategy and operator movement |
| Handover output | Validated cycle, tool list and maintenance plan |
Reduce setups with intent
Five-axis capability creates value when fixtures, probing and tool access are designed together for the part family.
Treat chips as a process
Coolant direction, chip evacuation and filtration should be considered during application review, not after installation.
Make the tool strategy visible
Tool life, measurement and replacement rules help production teams protect the expected cycle time.
Use the right acceptance sample
A realistic part and material are more useful than a theoretical cycle when the machine is being approved.
Train for recovery
Operators need clear recovery steps for alarms, probing deviations and tool changes so small stops stay small.